

『High-Temperature Steam Flow Meter Selection for Industrial Boiler Systems』Related information(flow rotameter|digital flow meter|balo meter|hydraulic flow meter|volumetric meter|positive displacement meter|pitot tube flow meter|displacement meter|cfm meter|variable area flow meter|inline flow meter|differential pressure flow meter|calibrated flow meter|velocity meter|paddle wheel flow meter|oval gear flow meter|anemometer hvac|multiphase flow meter|doppler flow meter|thorpe tube flowmeter|heat flow meter)
High-Temperature Steam Flow Meter Selection for Industrial Boiler Systems
Quick Answer: For high-temperature saturated or superheated steam in boiler systems, vortex flow meters offer the most reliable and cost-effective solution. They handle temperatures up to 350 °C, need no moving parts, and deliver mass flow directly when paired with built-in pressure and temperature compensation. Send your pipe size (DN), steam pressure (bar), and steam temperature (°C) to [email protected] for a same-day quote with lead time.
Why Steam Measurement Fails Without the Right Meter Type
Boiler steam flow measurement often fails because engineers pick a meter rated for water or gas. Steam is different. It changes density with every pressure and temperature swing. A 2 bar drop in a saturated steam line can shift the density by more than 10 percent. If the flow meter does not compensate for this shift, the readings become useless for energy management or billing. Silver Instruments supplies vortex flow meters with integrated PT100 temperature sensors and pressure transmitters. These units output mass flow in kg/h or t/h directly via a 4-20 mA HART signal. No separate flow computer is needed.
Many plants still run old orifice plate systems with impulse lines and differential pressure transmitters. These systems clog. They need constant purging and zero checks. Here is the thing. A vortex meter eliminates impulse lines entirely. You install a single inline device and get stable steam flow data within minutes of commissioning. We have seen this on customer sites many times.
Choosing Between Vortex, Orifice, and Thermal Mass for Boiler Steam
Vortex flow meters dominate mid-to-high temperature steam lines. They survive up to 350 °C with no drift in the bluff body signal. Silver Instruments vortex meters use a welded sensor design with no internal gaskets. This avoids leak paths common in flanged assemblies at 40 bar and 250 °C. The sensor is a piezo-accelerometer with a frequency output proportional to volumetric flow. Combined with a 4-20 mA HART multivariable transmitter, the same device gives mass flow for boiler efficiency monitoring.
Orifice plates still have a role. If a pipe is larger than DN300, a machined orifice carrier with a differential pressure transmitter is an option. However, the installation cost is higher. The pipe must be opened. Impulse tubing must be sloped correctly. For most boiler houses in Southeast Asia and Latin America, a wafer-style vortex meter from DN15 to DN300 is faster to install.
Thermal mass flow meters are not recommended for saturated steam. The condensate film on the sensor prevents accurate reading. Coriolis mass flow meters offer high accuracy on superheated steam but the price tag is rarely justified for a 4 t/h fire-tube boiler. Most engineers skip this part and choose vortex for a reason: it works and it lasts.
Key Selection Factors for Boiler Steam Flow Meters
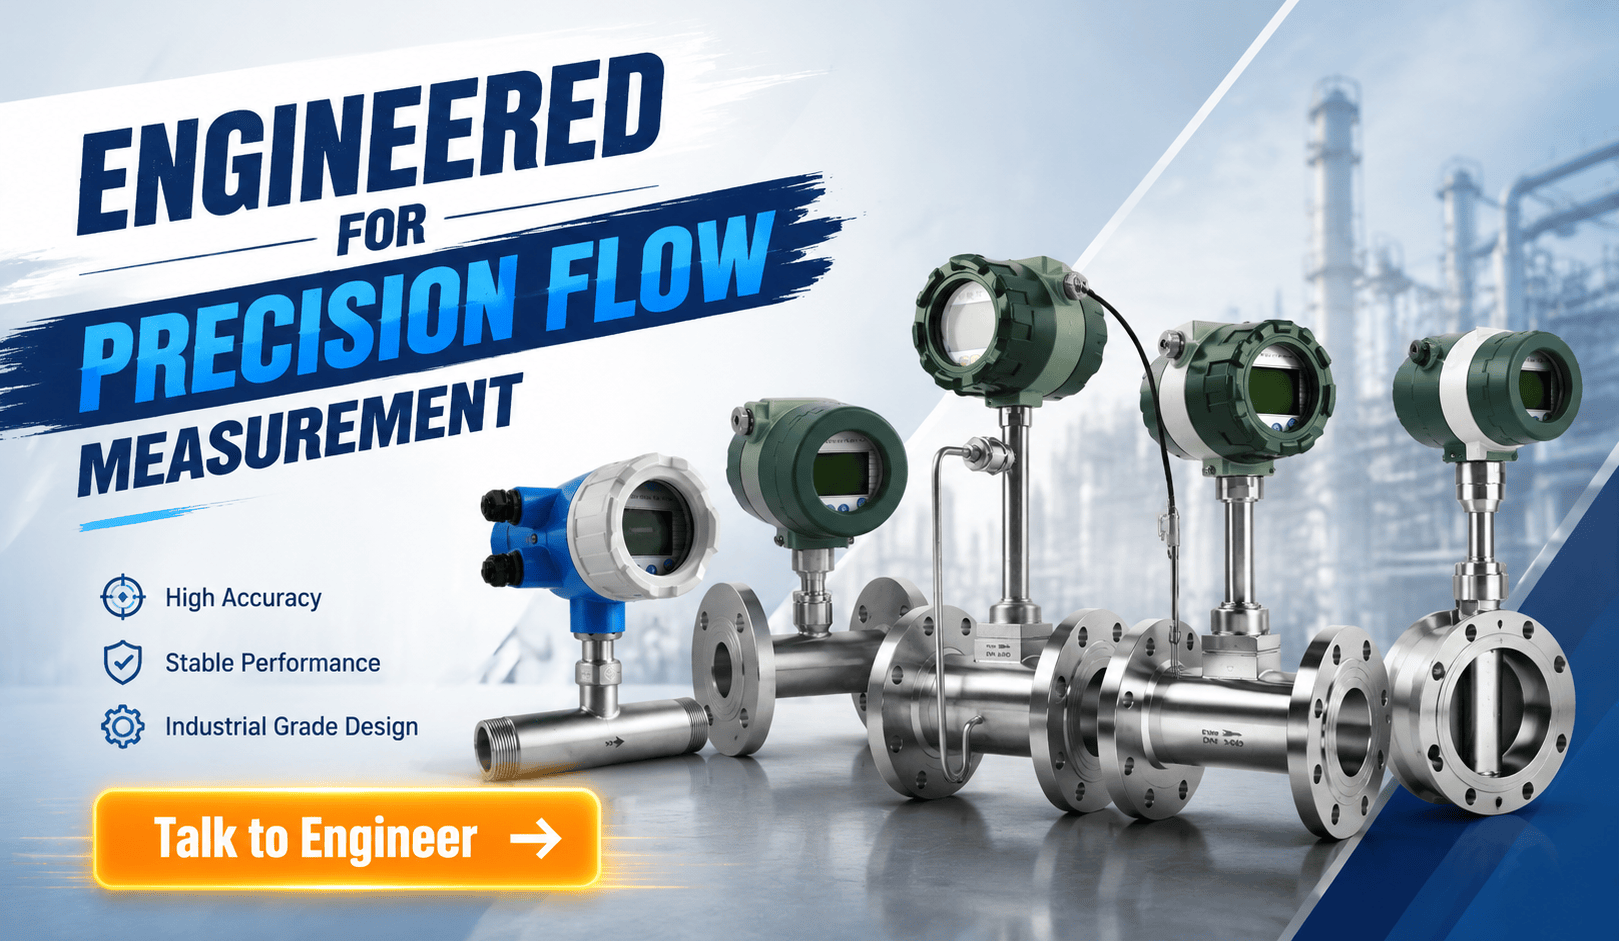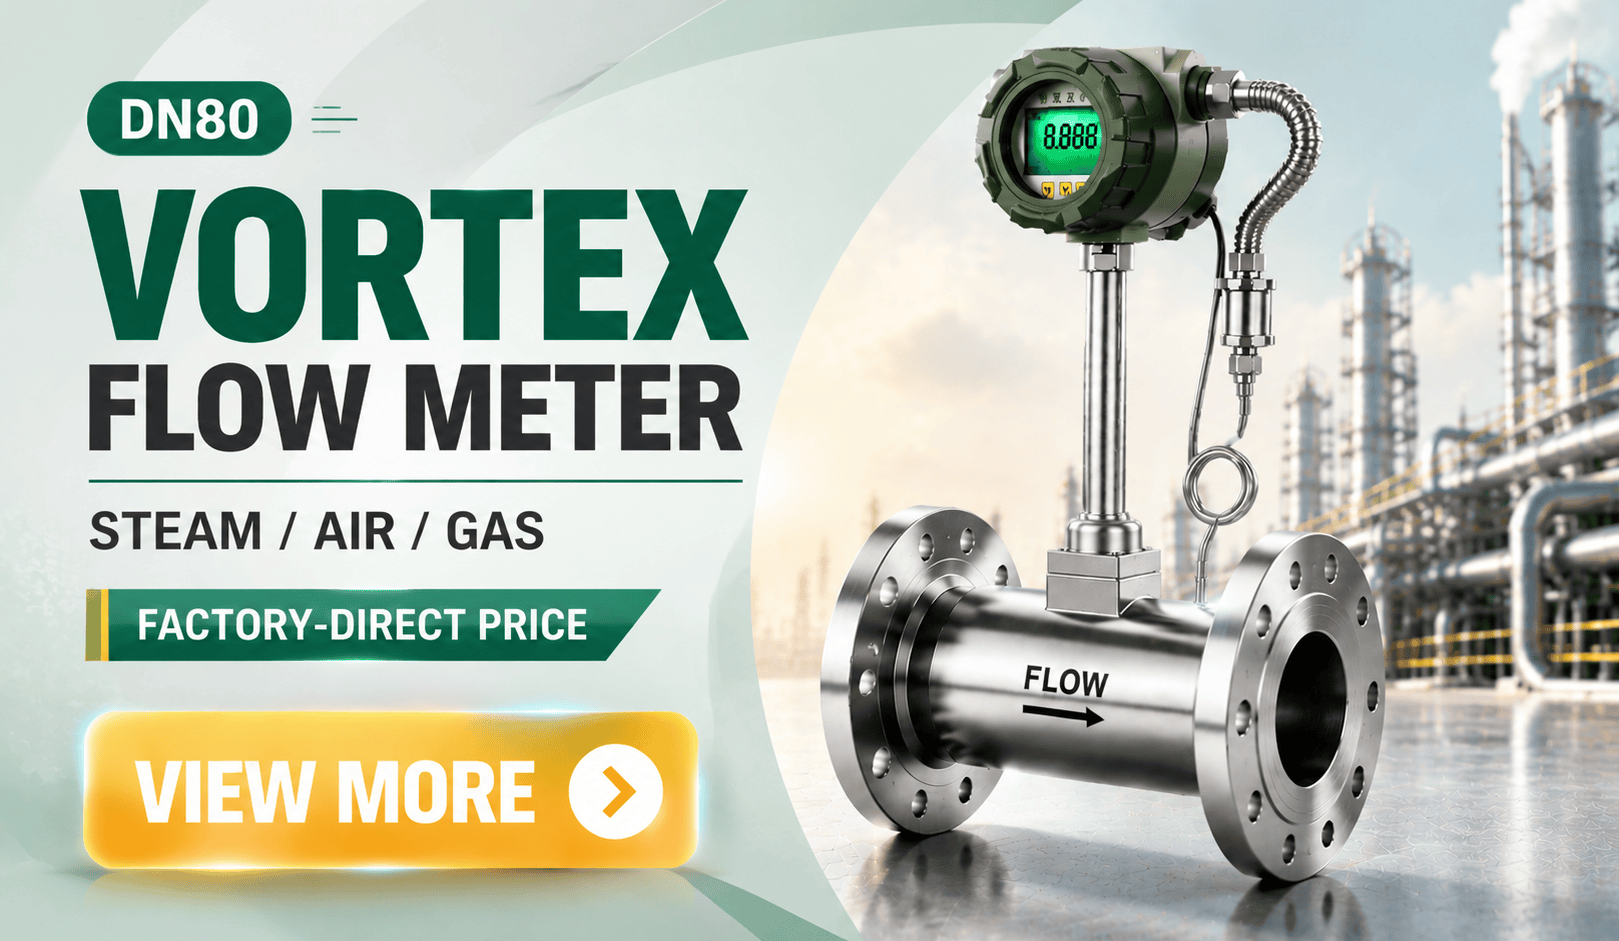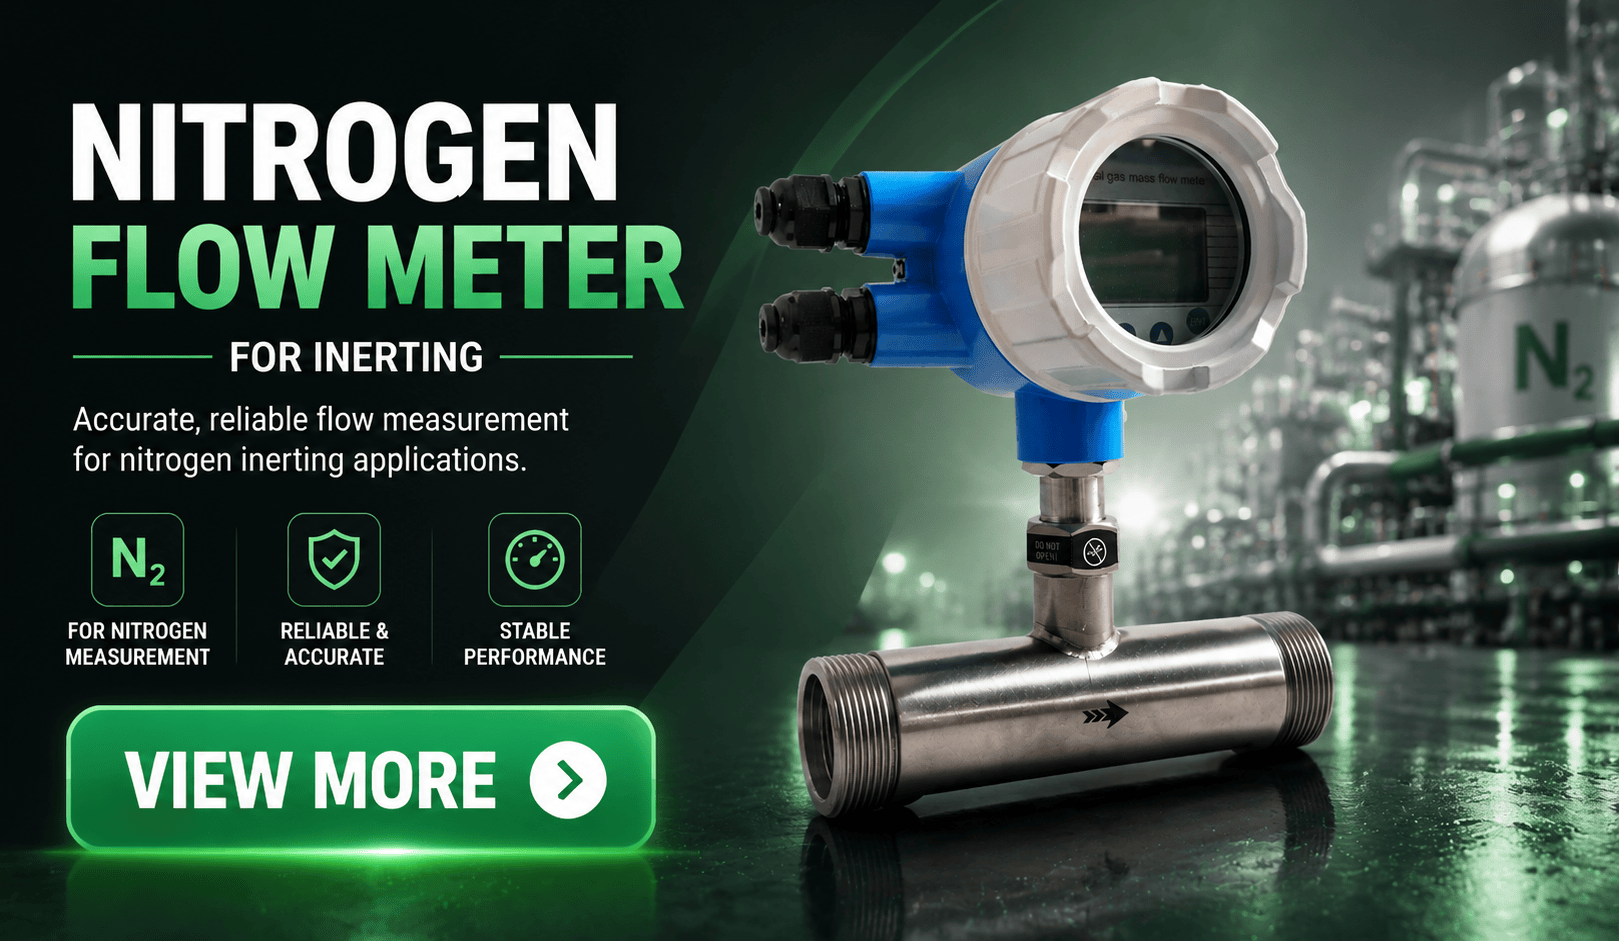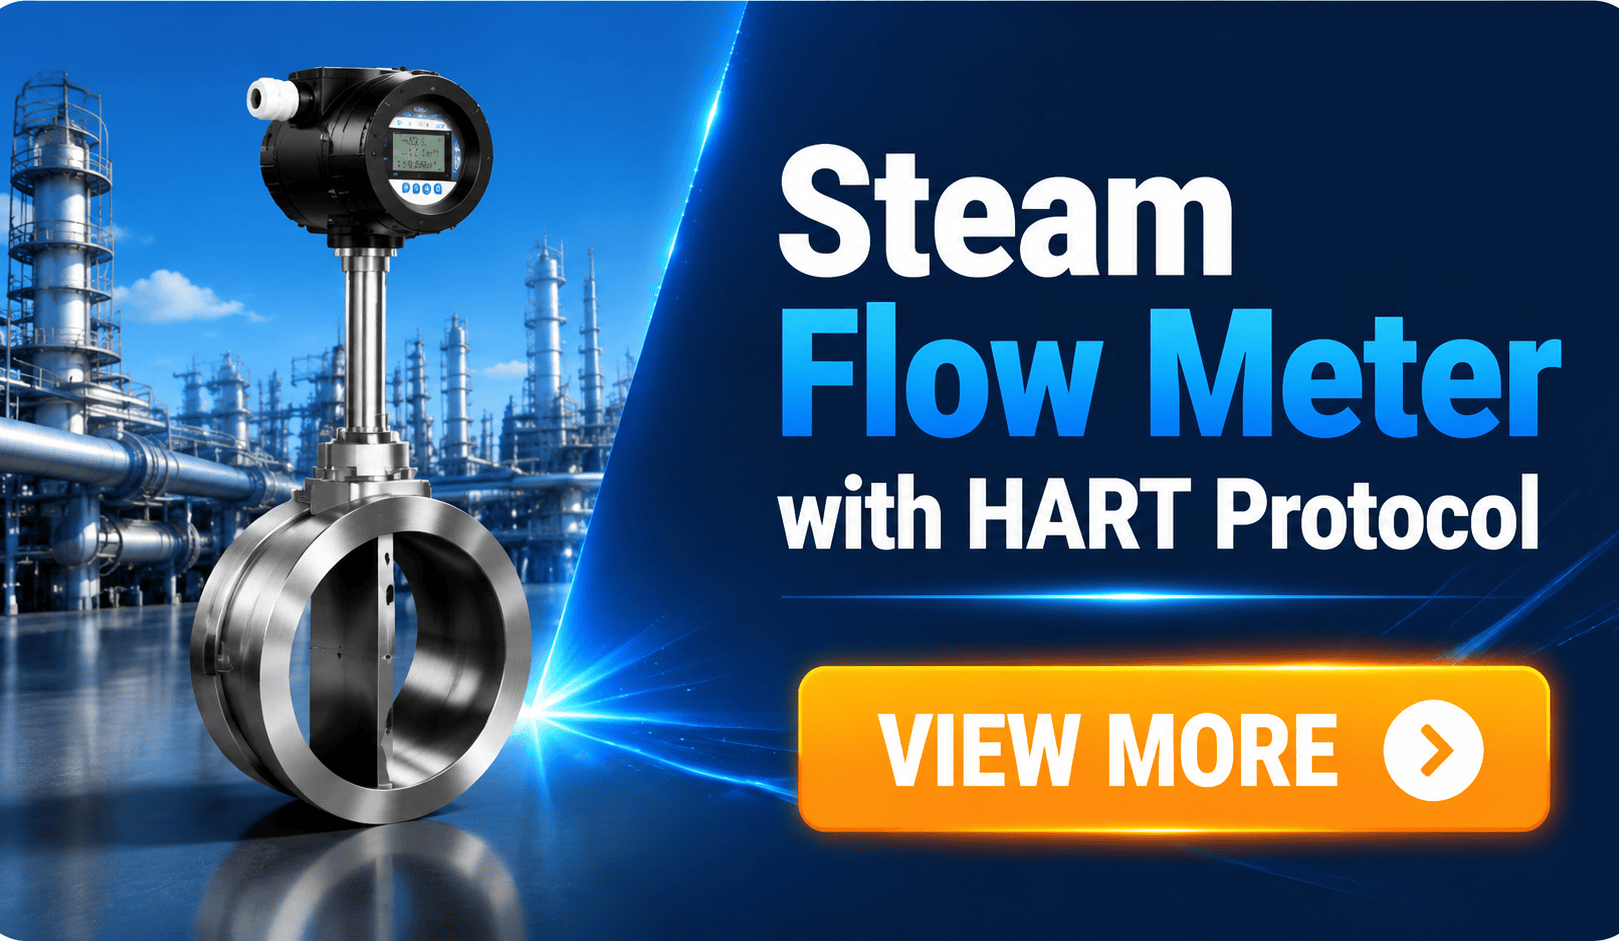
Pipe diameter is the first filter. Silver Instruments vortex meters cover DN15 to DN300. A typical industrial boiler in Thailand or Vietnam runs a DN80 or DN100 steam header. The flow range must match. Our DN80 vortex meter covers 60 to 1200 kg/h of saturated steam at 10 bar. That is enough for a 2-ton boiler.
Temperature and pressure ratings drive material selection. Sensor bodies are 316L stainless steel. Connection heads are available in aluminum or stainless steel. For superheated steam at 300 °C and 30 bar, we add a high-temperature heat sink extension. This protects the electronics from radiant heat. We have delivered over 50 such extensions to a boiler package supplier in Mexico last year.
Output signal is another decision. Many boiler control panels still accept a 4-20 mA pulse or analog signal. Silver Instruments vortex meters offer standard 4-20 mA HART, pulse output, and RS485 Modbus RTU. Modbus is growing fast in boiler monitoring systems across the Middle East. It allows the central PLC to read temperature, pressure, flow rate, and totalised flow on a single twisted pair.
Hazardous area certification matters more than some engineers think. A boiler house with a gas burner might be classified as ATEX Zone 2 or IECEx Zone 2
Installation Details That Prevent Measurement Errors
Steam flow meters need straight pipe upstream and downstream. For a vortex meter, the rule is 15D upstream and 5D downstream, where D is the pipe internal diameter. A boiler outage is a good time to check this. Many sites add a flow straightener if the pipe bend is too close. We supply perforated plate straighteners matched to the pipe schedule.
The meter must be installed after the steam trap and after the desuperheater, if one exists. Wet steam destroys the vortex signal. The steam quality at the meter location must be at least 95 percent dry. This is not a theory. It is a real issue in African breweries and Asian textile mills we support. When the boiler primes or carries water over, the flow meter output drops to zero. A properly located vortex meter with a drain pocket upstream solves this.
Condensate buildup in the electronics housing is another silent killer. Every Silver Instruments steam vortex meter comes with a cable gland rated IP67 and a conduit drain. We recommend mounting the transmitter below the pipe for steam, so condensate cannot travel back into the sensor neck. This simple trick extends meter life by years.
Maintenance and Long-Term Reliability in Boiler Houses
Vortex meters have no moving parts. The bluff body and sensor are fixed. Annual inspection means checking the sensor K-factor against a handheld communicator. No recalibration is needed unless the meter suffers physical damage. A boiler plant in Indonesia has six of our DN50 steam meters running 24/7 for four years without a single drift in K-factor. They check the meters every six months during boiler overhaul.
Orifice plate systems, on the other hand, need annual plate inspection and transmitter recalibration. The sharp edge of the orifice erodes over time. Steam is abrasive when it carries iron oxide particles from old carbon steel pipes. That erodes the orifice bore and shifts the DP relationship. A vortex meter is less sensitive to this wear because the bluff body is thicker.
Frequently Asked Questions
What flow meter types can handle steam above 300 °C?
Vortex flow meters with a high-temperature extension can measure steam up to 350 °C. Special welded orifice plates with remote diaphragm seals can go higher, but vortex is the simpler choice.
Can a Coriolis meter measure superheated steam?
Coriolis meters can measure superheated steam mass flow with high accuracy, but the material cost and pressure drop are not practical for most industrial boilers. We guide customers to vortex meters unless the application demands custody transfer accuracy.
Do I need temperature and pressure compensation for steam flow?
Yes. Without compensation, the output is only volumetric flow, which is meaningless for steam energy balance. Silver Instruments vortex meters include a built-in PT100 and pressure sensor with a multivariable transmitter, so they output compensated mass flow directly.
How fast can I get a DN100 steam flow meter shipped to Australia or Kenya?
Standard DN100 vortex meters are in stock at our Nanjing factory. We ship within 5 working days via UPS or DHL. Larger sizes or custom materials may take 2 to 3 weeks. Send your specs and we confirm stock and lead time within hours.
What signal output works best with a boiler PLC?
4-20 mA HART is the universal choice. If your boiler PLC has Modbus RTU capability, use RS485 Modbus output. You get flow, temperature, pressure, and totalised value on one cable pair. We pre-configure the registers so the connection is plug-and-play.
Tell us your steam conditions. We match the right meter on the first try. Email [email protected] or call us at +86-135-1213-1526. You can also reach us on WhatsApp at 86-135-12131526 or on WeChat at +86 13512131526. State your pressure (bar), temperature (°C), pipe size (DN), and normal flow range. We return the model number, price, and delivery estimate fast.
 Hot Product
 Related AD